Storage Automation Solutions: A Complete Guide for Modern Industries
Storage automation solutions are changing the way modern warehouses, manufacturing facilities, distribution centers, and industrial organizations store and retrieve materials. As businesses manage increasing inventory volumes and face pressure to use available space more efficiently, traditional manual storage methods can become difficult to scale.
Storage automation combines automated equipment, storage systems, sensors, control technology, software, and material handling equipment to make the storage and retrieval process faster, more organized, and more consistent.
From Automated Storage and Retrieval Systems (AS/RS) and automated pallet storage to conveyors, vertical storage systems, RGVs, AMRs, and intelligent control systems, storage automation can be designed around the specific requirements of a facility.
The objective is not simply to automate storage. A well-designed system should improve the complete material flow, from receiving and identification through storage, retrieval, production supply, picking, and dispatch.
This guide explains what storage automation solutions are, how they work, the major technologies involved, their benefits, applications across industries, implementation considerations, maintenance requirements, and future trends.
What Are Storage Automation Solutions?
Storage automation solutions are technologies and integrated systems used to automate the placement, storage, retrieval, movement, and tracking of materials within a warehouse or industrial facility.
In a conventional warehouse, employees may use forklifts, pallet trucks, shelves, racks, and manual records to store and retrieve products.
In an automated storage environment, equipment and software can perform many of these activities automatically.
A storage automation system can include:
- Automated Storage and Retrieval Systems
- Automated pallet storage
- Shuttle systems
- Vertical storage systems
- Conveyor systems
- RGV transportation
- AGVs
- AMRs
- Automated lifts
- Sensors and barcode systems
- RFID systems
- PLC and HMI controls
- Warehouse control software
- Warehouse management system integration
The final configuration depends on the type of material being stored, required storage capacity, throughput, warehouse layout, product dimensions, product weight, retrieval frequency, and operational requirements.
Why Is Storage Automation Important?
Warehouse space is an important operational resource. Businesses often need to store more inventory without continuously expanding their physical footprint.
Manual storage processes can also create challenges such as:
- Poor space utilization
- Longer retrieval times
- Inventory inaccuracies
- Excessive forklift movement
- Manual data-entry errors
- Product damage
- High dependence on manual handling
- Difficulty maintaining consistent processes
Storage automation can address many of these challenges by organizing storage locations and controlling material movement through automated processes.
A properly designed automated storage system can use vertical space more effectively, reduce unnecessary travel, improve inventory visibility, and create more predictable storage and retrieval processes.
How Do Storage Automation Solutions Work?
A typical automated storage process begins when material enters the warehouse.
The material is identified using a barcode, RFID tag, product number, or another identification method. The warehouse software determines where the material should be stored based on defined rules.
An automated transportation or storage system then moves the material to the assigned location.
When the material is required, the system receives a retrieval request. The appropriate automated equipment retrieves the material and delivers it to a predefined workstation, production area, picking location, or dispatch zone.
A simplified process is:
Receiving → Identification → Storage Assignment → Automated Storage → Inventory Tracking → Retrieval Request → Automated Retrieval → Delivery
The control system coordinates equipment, sensors, motors, drives, and software to complete these operations.
This creates a connected storage process rather than treating storage and material transportation as separate activities.
Main Components of Storage Automation Systems
1. Automated Storage and Retrieval Systems
Automated Storage and Retrieval Systems, or AS/RS, are among the most widely recognized storage automation technologies.
An AS/RS uses automated equipment to place and retrieve products from predefined storage locations.
Depending on the application, AS/RS can handle:
- Pallets
- Cartons
- Totes
- Bins
- Components
- Small parts
- Heavy industrial products
AS/RS systems can improve storage density and reduce manual travel within the warehouse.
2. Automated Pallet Storage
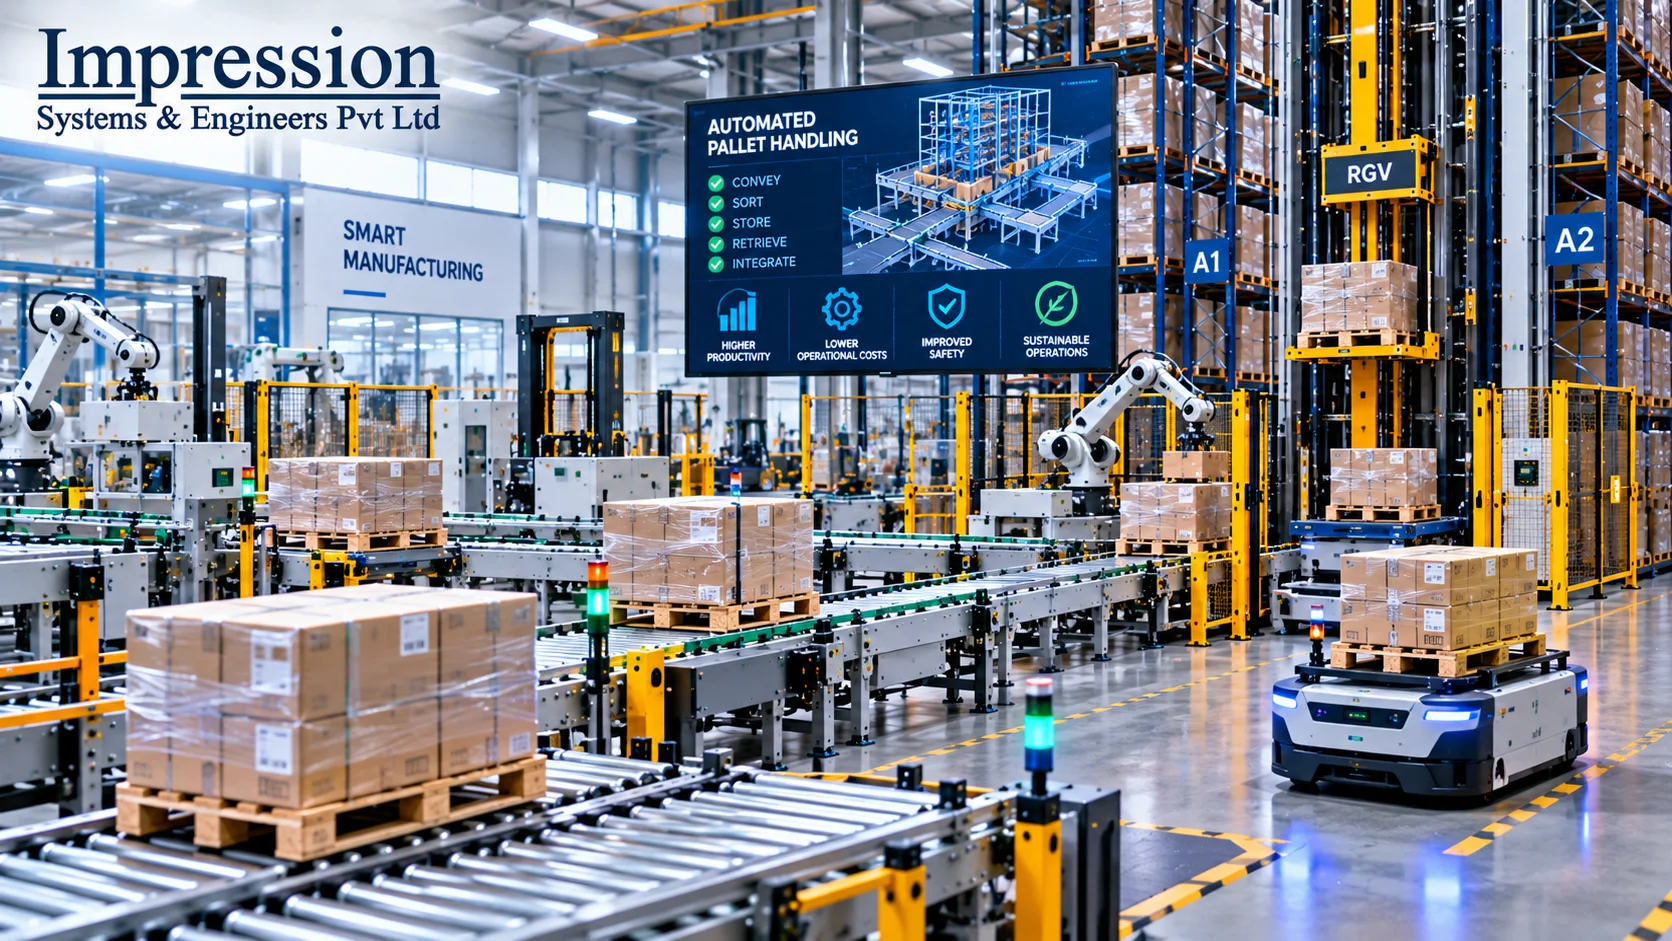
Automated pallet storage systems are designed for facilities handling large and heavy loads.
A typical system may combine:
- Pallet conveyors
- Storage racks
- Automated storage machines
- Transfer systems
- Lifts
- Sensors
- Control software
These systems can automate the movement of pallets between receiving, storage, production, and dispatch areas.
3. Conveyor Systems
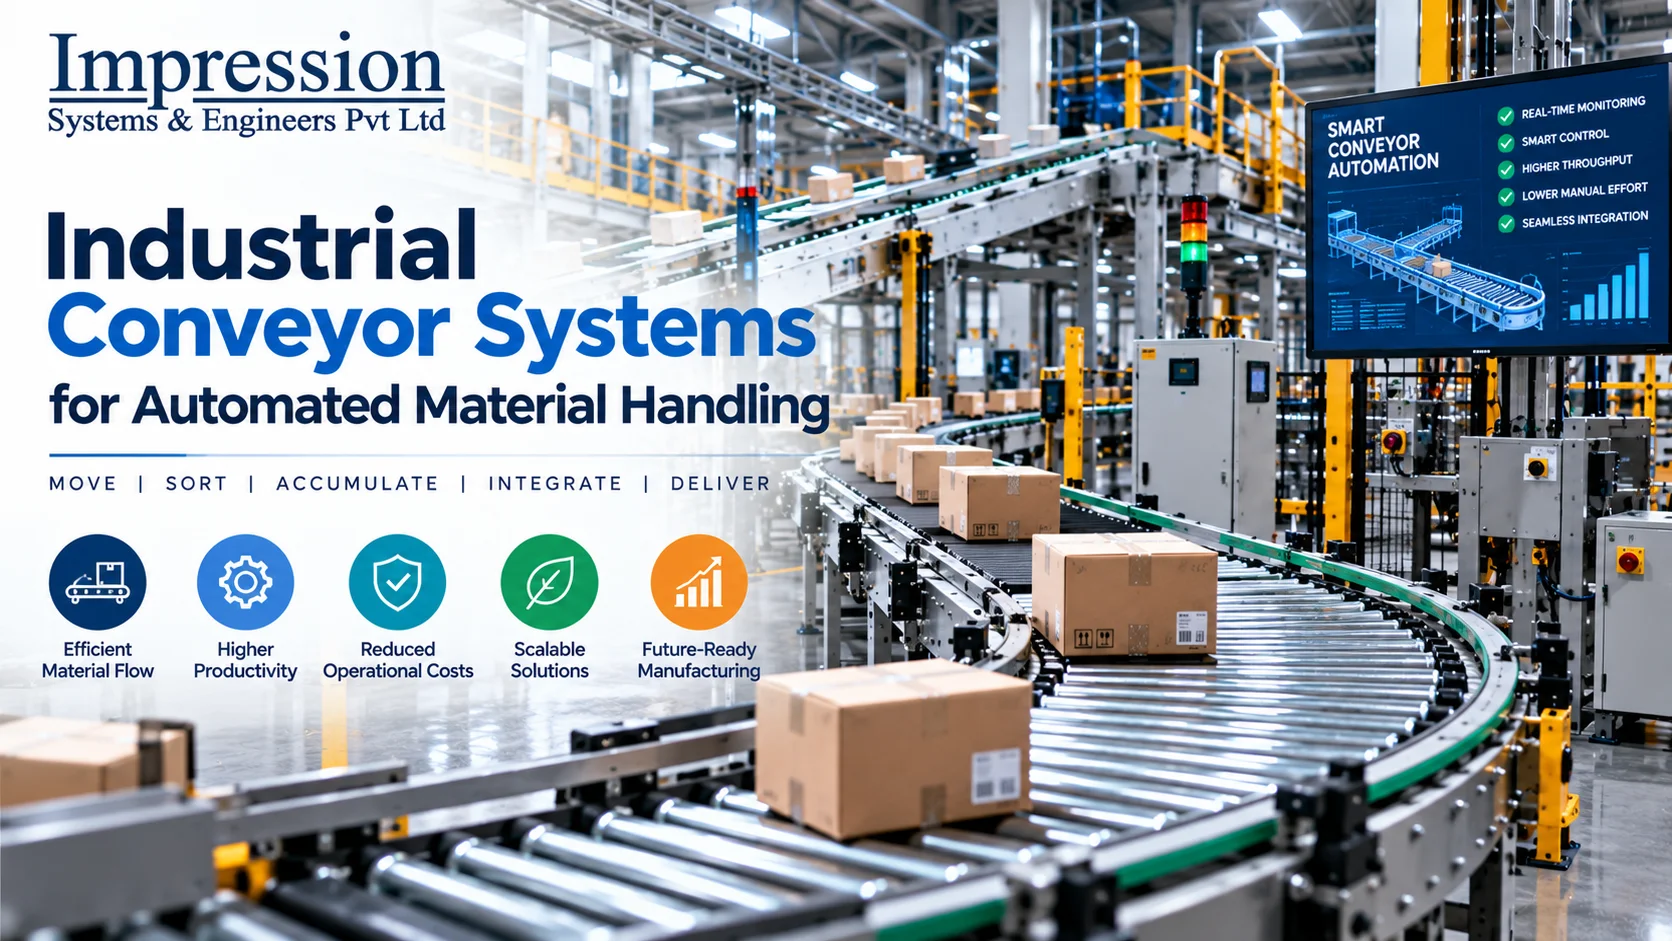
Conveyors provide automated transportation between storage locations and other warehouse zones.
Common types include:
- Roller conveyors
- Belt conveyors
- Chain conveyors
- Pallet conveyors
- Slat conveyors
- Transfer conveyors
- Accumulation conveyors
- Vertical conveyors
Conveyor systems can be integrated with AS/RS, picking stations, production lines, and dispatch systems.
4. Vertical Storage Systems
Vertical storage automation uses building height to increase storage capacity.
Vertical systems may include automated lifts or vertical storage machines that bring products to an operator or designated access point.
They can be useful when floor space is limited but sufficient building height is available.
5. Rail Guided Vehicles
Rail Guided Vehicles, commonly called RGVs, operate on fixed rail tracks.
They can transport pallets, containers, components, and other materials between predefined locations.
RGV systems can provide controlled and repeatable transportation within automated storage environments.
6. Automated Guided Vehicles
AGVs are automated vehicles that transport materials along predefined or controlled routes.
They can connect:
- Receiving areas
- Storage zones
- Production areas
- Picking stations
- Dispatch areas
AGVs can reduce repetitive manual transportation.
7. Autonomous Mobile Robots
AMRs use sensors, navigation technology, and software to move materials through dynamic environments.
AMRs can support:
- Tote movement
- Goods-to-person operations
- Order picking
- Replenishment
- Internal transportation
- Material transfer
They can be particularly useful where routes and workflows need flexibility.
8. Sensors and Identification Technology
Automated storage systems rely on accurate information.
Technologies can include:
- Barcode scanners
- RFID
- Photoelectric sensors
- Proximity sensors
- Vision systems
- Encoders
- Load sensors
- Position sensors
These devices help identify products, confirm positions, detect movement, and support equipment control.
9. PLC and HMI Controls
PLCs coordinate automated equipment and execute programmed sequences.
HMIs provide operators with a visual interface for monitoring and controlling the system.
A well-designed control system can display:
- Equipment status
- Storage status
- Alarms
- Fault information
- Operating modes
- Manual controls
- Maintenance information
10. Warehouse Control and Management Software
Software connects storage processes with business operations.
A Warehouse Management System can manage inventory and storage information, while a Warehouse Control System can coordinate automated equipment.
Integration can provide:
- Storage location management
- Retrieval instructions
- Inventory updates
- Equipment commands
- Order information
- System monitoring
- Operational reporting
Major Types of Storage Automation Solutions
Automated Pallet Storage
Automated pallet storage is suitable for heavy-duty warehouse applications.
It can provide controlled storage and retrieval while reducing forklift movement.
Typical applications include:
- Manufacturing warehouses
- Distribution centers
- Automotive facilities
- Food and beverage warehouses
- Industrial storage
- Finished goods warehouses
Mini-Load AS/RS
Mini-load systems are designed for smaller products, bins, cartons, and totes.
They can support high-density storage where many smaller items must be stored and retrieved efficiently.
Shuttle-Based Storage
Shuttle systems use automated vehicles to move products within storage lanes.
They can provide high-density storage and are useful in applications with repetitive storage and retrieval patterns.
Vertical Storage Automation
Vertical systems maximize the use of available building height.
They can be suitable for small components, spare parts, tools, and other products requiring organized storage and controlled access.
Automated Buffer Storage
Buffer storage systems temporarily hold products between different processes.
For example, a warehouse may use automated buffer storage between production and dispatch to balance variations in process speed.
Dynamic Automated Storage
Dynamic systems use software and automated equipment to determine and manage storage locations according to operational requirements.
This can help improve utilization and retrieval efficiency.
Benefits of Storage Automation Solutions
Better Space Utilization
One of the major advantages of storage automation is the ability to use available vertical and floor space efficiently.
Automated storage systems can reduce unnecessary aisle space and organize products into controlled storage locations.
Higher Storage Capacity
Businesses may be able to store more products within an existing facility by using high-density and vertical storage solutions.
Improved Inventory Accuracy
Automated identification and software-based storage management can reduce errors associated with manual inventory recording.
Faster Retrieval
Automated equipment can retrieve products from known locations without requiring operators to manually search through storage areas.
Reduced Manual Handling
Automation can reduce repetitive lifting, carrying, and forklift transportation.
Improved Workplace Ergonomics
Reducing repetitive physical movement can help create more ergonomic work environments when the system is properly designed.
Better Traceability
Automated systems can record storage and retrieval activities, making it easier to track material movement.
Reduced Product Damage
Controlled transportation and storage can reduce certain types of damage associated with manual handling.
Better Operational Consistency
Automated processes follow predefined sequences and rules, helping create predictable storage and retrieval operations.
Scalability
Automation can be designed with future expansion in mind, allowing additional storage capacity or transportation systems to be added when business requirements increase.
Storage Automation Applications Across Industries
Automotive Industry
Automotive manufacturing requires efficient storage and supply of components, assemblies, tools, and production materials.
Storage automation can support:
- Component storage
- Palletized parts
- Production sequencing
- Line-side material supply
- Returnable container storage
- Finished goods
- Spare parts
Automated transportation systems such as RGVs, conveyors, AMRs, and AS/RS can connect storage with production.
Food and Beverage Industry
Food and beverage operations can use automated storage systems for raw materials, packaging, finished products, and distribution inventory.
Potential applications include:
- Pallet storage
- Carton storage
- Inventory tracking
- Automated retrieval
- Dispatch preparation
- FIFO and FEFO workflows where required
Pharmaceutical Industry
Pharmaceutical storage requires accurate identification and controlled inventory management.
Automation can support:
- Small-item storage
- Batch identification
- Inventory tracking
- Order retrieval
- Controlled material movement
- Storage location management
Electronics Industry
Electronics warehouses often contain large numbers of small components.
Mini-load systems, vertical storage, automated picking, barcode identification, and controlled material handling can help manage these inventories.
Appliances Industry
Appliance warehouses often handle bulky finished products and components.
Automated pallet handling, conveyors, storage systems, and transportation automation can help improve internal material flow.
Metal and Engineering Industry
Heavy-duty storage automation can support metal and engineering operations where products and components may be heavy or difficult to handle manually.
Solutions can be designed for:
- Heavy pallets
- Components
- Fabricated parts
- Work-in-progress
- Finished products
- Industrial materials
Logistics and Distribution
Distribution centers need to process large product volumes while maintaining accurate inventory records.
Storage automation can support:
- High-density storage
- Automated retrieval
- Order fulfillment
- Inventory tracking
- Sortation
- Dispatch preparation
Storage Automation and Industry 4.0
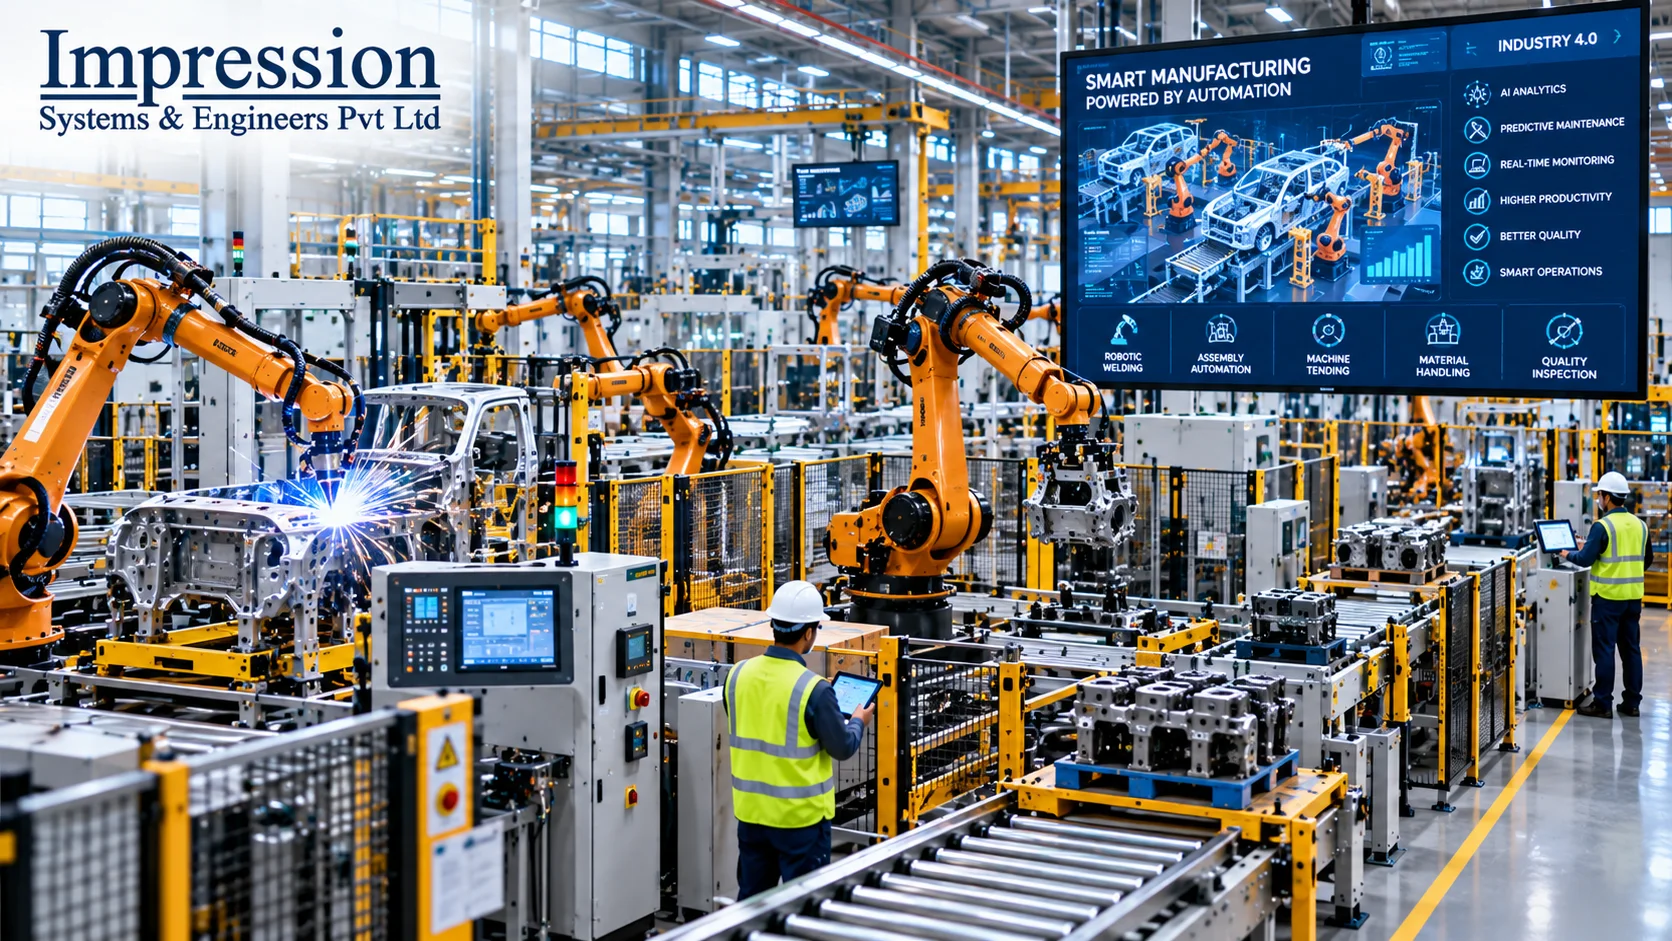
Industry 4.0 is making storage systems increasingly connected and data-driven.
Modern storage automation can incorporate:
- Industrial IoT
- Artificial intelligence
- Machine learning
- RFID
- Computer vision
- Cloud monitoring
- Data analytics
- Digital twins
- Predictive maintenance
- Robotics
Connected storage systems can provide information about inventory, equipment condition, throughput, and operational performance.
For example, equipment sensors can provide data about motor temperature, vibration, operating cycles, and other parameters. This information can support predictive maintenance programs.
Data analytics can also identify bottlenecks and help organizations understand how storage and retrieval processes perform during different operating conditions.
Integration with WMS and ERP Systems
Storage automation should not operate as an isolated system.
Integration with a Warehouse Management System allows inventory and storage information to be coordinated with automated equipment.
ERP integration can connect warehouse activities with broader business processes.
A connected architecture may include:
ERP ↔ WMS ↔ WCS ↔ PLC ↔ Automated Equipment
The exact architecture depends on the project.
Integration can provide:
- Real-time inventory information
- Storage location updates
- Automated retrieval instructions
- Order information
- Equipment status
- Production requirements
- Dispatch information
Effective integration is important because automation equipment needs accurate instructions and the business needs reliable information about inventory.
How to Choose the Right Storage Automation Solution
Choosing the correct technology requires a detailed assessment.
Understand the Products
Analyze:
- Product dimensions
- Weight
- Shape
- Packaging
- Fragility
- Storage conditions
- Identification requirements
Analyze Storage Requirements
Determine:
- Current inventory
- Maximum inventory
- Required storage locations
- Product turnover
- Retrieval frequency
- Seasonal fluctuations
Calculate Throughput
Understand how many storage and retrieval transactions are required during:
- Normal operation
- Peak operation
- Seasonal demand
- Production peaks
Study the Facility
Review:
- Floor area
- Ceiling height
- Rack configuration
- Structural limitations
- Loading areas
- Production interfaces
- Existing equipment
Define Software Requirements
Determine how the automation system needs to communicate with:
- WMS
- ERP
- MES
- Barcode systems
- RFID systems
- Production systems
Consider Future Growth
The storage solution should consider future inventory growth, additional products, changing customer requirements, and potential warehouse expansion.
Customized Storage Automation Solutions
Not every facility can use a standard storage system.
Customized storage automation may be necessary when a warehouse has:
- Unusual building dimensions
- Heavy products
- Irregular product shapes
- Limited floor space
- High ceilings
- Multi-level storage
- Complex material flow
- Existing automation
- Specialized production requirements
A customized solution normally starts with process analysis and layout planning.
The automation provider can then develop the appropriate mechanical, electrical, software, and control architecture.
Storage Automation Implementation Process
1. Requirement Study
The first stage is understanding the existing operation.
The study should cover:
- Product characteristics
- Inventory
- Throughput
- Material flow
- Storage requirements
- Existing systems
- Future requirements
2. Concept Development
The automation concept defines the proposed storage technology, material flow, equipment, and software architecture.
3. Layout and Engineering
Detailed mechanical, electrical, controls, safety, and software engineering is performed.
4. Manufacturing
The required equipment and assemblies are manufactured according to the approved design.
5. Installation
Equipment is installed and integrated at the facility.
6. Testing and Commissioning
Testing verifies:
- Equipment operation
- Sensors
- Controls
- Safety systems
- Communication
- Storage and retrieval
- Material flow
- Software integration
7. Training and Handover
Operators and maintenance personnel are trained in system operation, safety, troubleshooting, and preventive maintenance.
Maintenance of Storage Automation Systems
Maintenance is essential for long-term system reliability.
Typical preventive maintenance activities include:
- Conveyor inspection
- Motor inspection
- Sensor inspection
- Chain and roller checks
- Lubrication
- Electrical panel inspection
- Safety device testing
- PLC backup
- Software backup
- RGV or AMR inspection
- Storage equipment inspection
Predictive maintenance can further improve reliability by monitoring equipment conditions and identifying potential failures before they become major operational problems.
A maintenance program should also include appropriate spare parts, technical support, inspection schedules, and emergency response procedures.
Common Mistakes When Implementing Storage Automation
Choosing Technology Before Understanding the Process
The technology should follow the operational requirement. Businesses should first understand their material flow and storage challenges.
Ignoring Peak Throughput
Designing only for average demand can create bottlenecks during peak periods.
Underestimating Integration
Automation equipment must exchange information correctly with WMS, ERP, and other systems.
Not Considering Future Expansion
A system designed without future requirements may become difficult to expand.
Ignoring Product Characteristics
Product weight, dimensions, packaging, fragility, and storage requirements should influence equipment selection.
Inadequate Training
Operators and maintenance personnel need appropriate training before operating automated systems.
Poor Maintenance Planning
Preventive and predictive maintenance should be considered from the beginning of the project.
Future Trends in Storage Automation
Storage automation will continue to evolve as warehouses become more connected and intelligent.
AI-Based Optimization
Artificial intelligence can support inventory planning, storage allocation, retrieval prioritization, and demand forecasting.
Robotics
Robotic systems can support picking, palletizing, transportation, and other warehouse activities.
Computer Vision
Vision technology can improve product identification, inspection, counting, and robotic handling.
Digital Twins
Digital twins can simulate warehouse layouts and material flow before physical changes are implemented.
Predictive Maintenance
Connected sensors can provide early indications of equipment degradation.
Cloud-Based Monitoring
Cloud platforms can provide remote access to equipment performance and operational information.
Flexible Automation
AMRs and other flexible automation technologies can help warehouses adapt to changing layouts and product requirements.
Why Choose an Experienced Storage Automation Partner?
Storage automation involves several engineering disciplines.
A successful project may require expertise in:
- Mechanical engineering
- Electrical engineering
- Automation controls
- PLC programming
- HMI development
- Software integration
- Safety systems
- Material flow
- Warehouse processes
- Installation
- Commissioning
- Maintenance
An experienced partner can evaluate the complete process instead of recommending isolated equipment.
This integrated approach helps ensure that storage, transportation, controls, software, and business processes work together.
Storage Automation Solutions from Imensys
Imensys works in industrial automation and material handling, supporting solutions designed to improve storage, transportation, and internal material flow.
Depending on the application, storage automation projects can incorporate technologies such as:
- Automated storage systems
- Material handling systems
- Conveyor systems
- RGV transportation
- AMR-based material movement
- Vertical transportation
- PLC and HMI control systems
- Customized automation
- System integration
The right storage automation solution should be selected after evaluating the facility, product characteristics, storage capacity, throughput, material flow, existing infrastructure, and future requirements.
For organizations looking to improve storage efficiency and automate repetitive material handling processes, a structured technical assessment can identify suitable automation opportunities.
Frequently Asked Questions About Storage Automation Solutions
What are storage automation solutions?
Storage automation solutions are systems that automate the storage, retrieval, movement, identification, and tracking of materials in warehouses and industrial facilities.
What is the most common storage automation technology?
AS/RS is one of the most widely recognized storage automation technologies, but the appropriate technology depends on product type, storage requirements, throughput, and facility design.
What are the benefits of storage automation?
Storage automation can improve space utilization, inventory accuracy, retrieval speed, material flow, traceability, workplace ergonomics, and operational consistency.
What is AS/RS?
AS/RS stands for Automated Storage and Retrieval System. It uses automated equipment to store and retrieve materials from designated locations.
Can storage automation work with an existing WMS?
Yes. Storage automation can be integrated with a WMS so that inventory information, storage locations, orders, and automated equipment can communicate.
Is storage automation suitable for manufacturing plants?
Yes. Manufacturing plants can use storage automation for raw materials, components, work-in-progress, finished products, spare parts, and production line replenishment.
Can storage automation increase warehouse capacity?
It can increase effective storage capacity by improving space utilization, using vertical space, and reducing unnecessary aisle and access requirements, depending on the facility and system design.
What is the difference between AS/RS and conventional storage?
Conventional storage generally relies more heavily on manual equipment and operator-driven storage and retrieval. AS/RS uses automated equipment and software to perform these activities.
How should a company start a storage automation project?
The project should begin with a detailed analysis of products, inventory, storage requirements, throughput, warehouse layout, material flow, existing systems, and future growth.
Conclusion
Storage automation solutions provide businesses with a way to transform conventional storage operations into more organized, connected, and efficient systems.
Technologies such as AS/RS, automated pallet storage, conveyors, vertical storage, RGVs, AGVs, AMRs, sensors, PLCs, and warehouse software can be combined according to the specific requirements of a facility.
The best solution is not necessarily the most technologically complex system. It is the system that effectively addresses the warehouse’s storage capacity, product characteristics, throughput, material flow, space limitations, safety requirements, and future business needs.
With proper planning, engineering, integration, commissioning, training, and maintenance, storage automation can become an important part of modern warehouse and industrial operations.
For businesses considering automation, the best starting point is a detailed assessment of the current storage process and identification of the specific operational improvements that automation should deliver.